

Pine Oil (No. 2 Frother): The Industry-Standard Frothing Agent for Mineral Flotation
Application Scope
Pine oil, also known as No. 2 flotation oil, is a widely used frother in non-ferrous metal flotation operations. It functions primarily by generating stable, fine bubbles that improve the transportation and recovery of hydrophobic mineral particles in flotation circuits. Its applications cover multiple strategic mineral processing operations, including sulfide and non-sulfide ore beneficiation.
Copper-Molybdenum Flotation
The most significant application of pine oil is in copper-molybdenum sulfide ore flotation. As a primary frothing agent, it produces stable and persistent froth that supports the recovery of hydrophobic sulfide minerals.
In porphyry copper-molybdenum flotation circuits, pine oil generates fine and dense bubbles capable of carrying chalcopyrite and molybdenite particles under high pulp density conditions. Its established performance in sulfide flotation also extends to copper, lead, zinc, and iron sulfide processing applications.
Gold Ore Flotation
In gold flotation circuits, pine oil acts as a frothing reagent for recovering gold-bearing sulfide minerals. It promotes air bubble dispersion in the flotation pulp, allowing gold-associated pyrite and arsenopyrite particles to attach to bubbles and transfer into concentrate streams.
Compared with stronger frothers, pine oil can provide balanced froth stability with reduced tendency for excessive slime entrainment, supporting selective flotation performance in suitable gold processing conditions.
Antimony and Tin Ore Processing
Pine oil is also applied in antimony beneficiation and tin ore processing, where consistent bubble characteristics are required across different flotation conditions. Its adaptability allows application in various sulfide and non-sulfide mineral circuits.
Lithium and Nickel-Cobalt Flotation Applications
In lithium pegmatite flotation, particularly spodumene beneficiation, pine oil serves as a frothing agent in conventional flotation and flotation column circuits. Its low water solubility helps maintain stable bubble films in the presence of fine slimes commonly found in lithium ores.
For nickel sulfide flotation, pine oil provides the froth generation required for recovering pentlandite from pyrrhotite-bearing ores.
Beyond these applications, pine oil may also exhibit moderate collecting properties for naturally hydrophobic minerals including talc, graphite, sulfur, molybdenite, and coal.
Mechanism
Pine oil is primarily composed of terpene alcohols, with α-terpineol as a major component. As a surface-active flotation reagent, it reduces surface tension at the gas-liquid interface and improves bubble formation within flotation pulp.
During flotation, pine oil molecules orient at the bubble surface, with nonpolar hydrocarbon groups directed toward the gas phase and polar hydroxyl (-OH) groups interacting with the aqueous phase. This creates a more elastic bubble film that helps reduce bubble coalescence and maintain froth stability.
Terpenic oil components may also adsorb onto certain mineral surfaces, increasing surface hydrophobicity and supporting particle-bubble attachment through hydrophobic interaction mechanisms.
Physicochemical Properties
| Parameter | Specification |
|---|---|
| CAS Number | 8002-09-3 |
| Molecular Formula | C₁₀H₁₇OH (predominant component) |
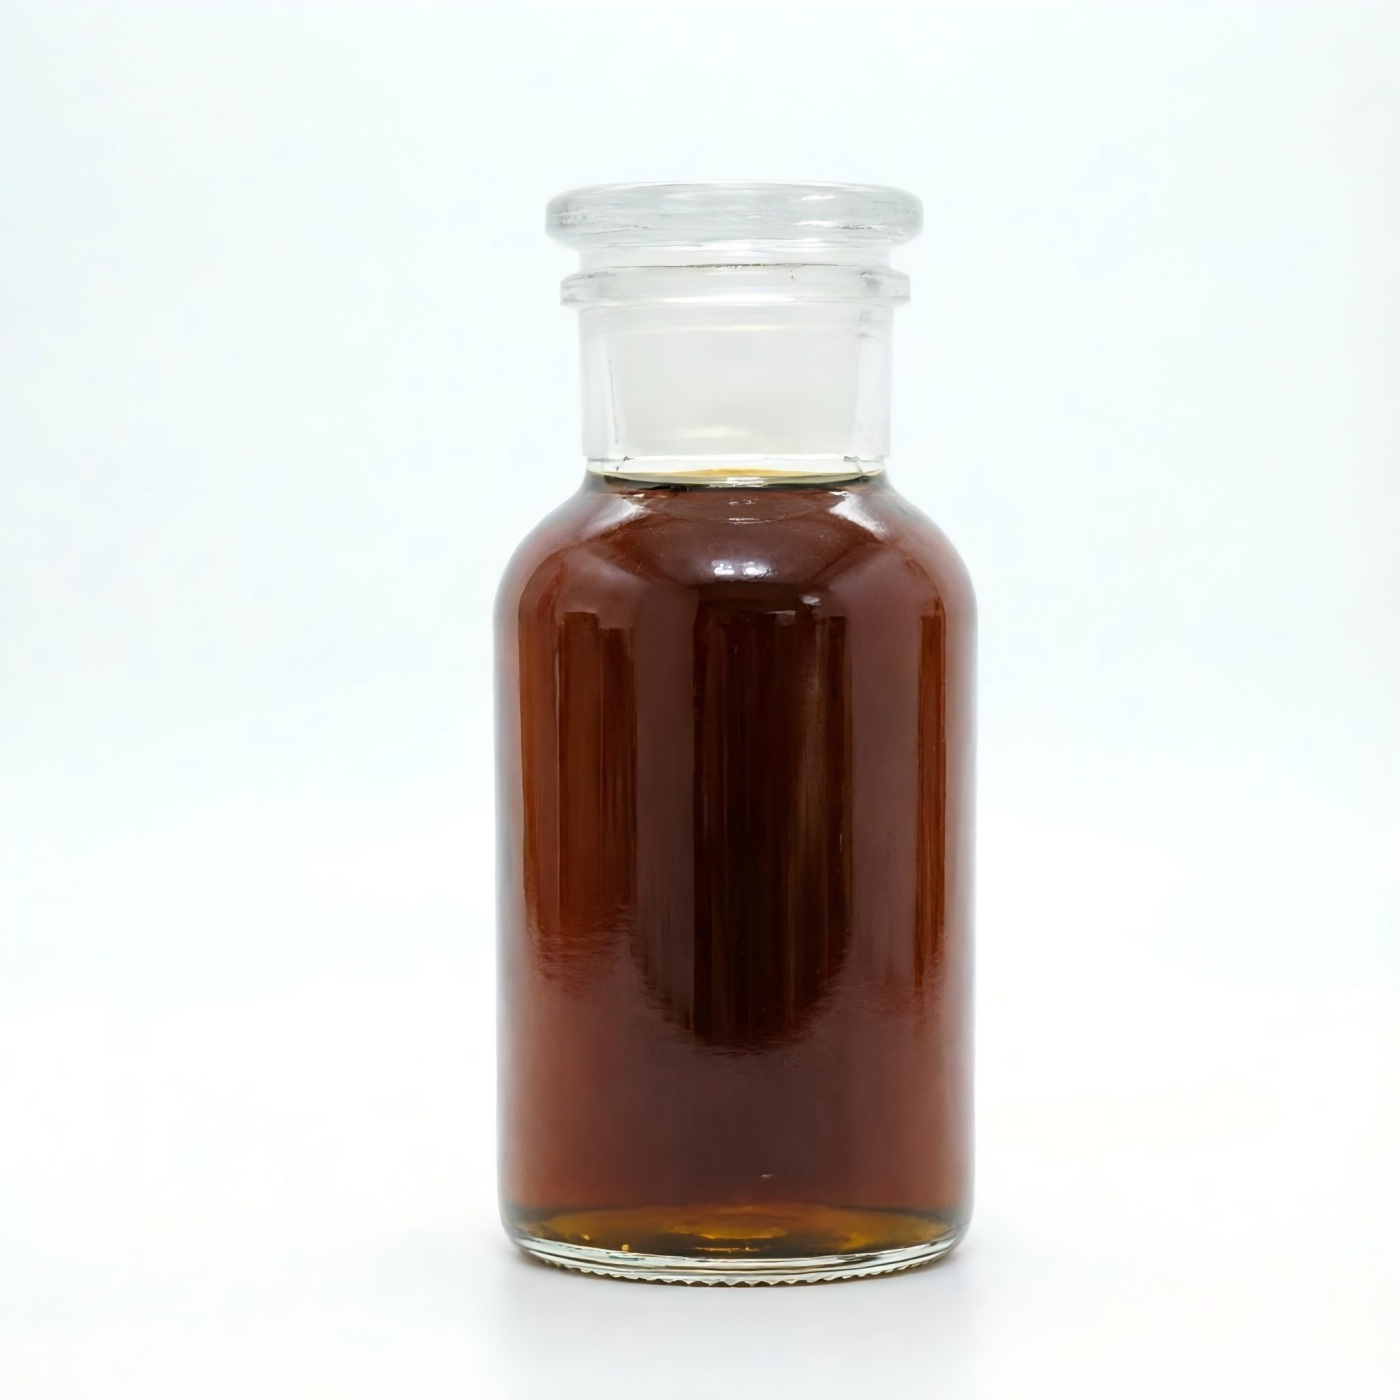
| Appearance | Yellow to brown oil liquid |
| Density | 0.90–0.92 g/cm³ |
| Terpene Alcohol Content | 40–50% (grade dependent) |
| Solubility | Slightly soluble in water |
Specifications
Pine oil grades are commonly differentiated by terpene alcohol content. Selection should consider flotation circuit requirements, mineral characteristics, and operational conditions.
Storage & Handling
Store pine oil in tightly sealed containers in a cool, dry, and well-ventilated area away from ignition sources. As a Class 3 flammable liquid, it should be kept separated from oxidizing agents and open flames.
Operators handling pine oil should use appropriate personal protective equipment, including chemical-resistant gloves, safety goggles, and protective clothing. Any spills should be contained with inert absorbent materials and managed according to local environmental regulations.
Advantages / Limitations
Advantages
Cost-effective frother with established supply availability.
Produces stable froth with resistance to bubble coalescence.
Provides moderate collecting properties for naturally hydrophobic minerals.
Suitable for various sulfide and non-sulfide flotation circuits.
Demonstrated application experience across multiple strategic mineral processing operations.
Limitations
May provide lower froth selectivity compared with MIBC in certain flotation applications.
Performance may be affected by acid or heat exposure conditions.
Used primarily as a frother and is not suitable as a standalone collector.
Different terpene alcohol grades require proper selection according to flotation requirements.
Summary
Pine oil (CAS 8002-09-3), also known as No. 2 flotation oil, is an established frother used in mineral flotation operations. Its primary applications include copper-molybdenum, gold, antimony, and tin flotation circuits, with additional applications in lithium and nickel sulfide beneficiation.
Containing terpene alcohol components with a density range of 0.90–0.92 g/cm³, pine oil generates stable fine bubbles by reducing interfacial tension in flotation pulp. Available in different grades with 40–50% terpene alcohol content, it provides a practical frothing solution for mineral processing operations when selected according to circuit conditions. Proper storage and handling procedures are required due to its Class 3 flammable liquid classification.
Pine Oil (No.2 Oil) – FAQ
Q1. What is the recommended dosage range of Pine Oil as a frother in flotation operations?
The dosage of Pine Oil (No.2 Oil) as a frother depends on ore properties, slurry conditions, and the flotation circuit design. In industrial practice, dosage is commonly optimized through laboratory flotation tests by evaluating froth stability, bubble size distribution, concentrate grade, and recovery performance. Factors such as pulp density, particle size, collector type, and water quality can significantly influence the required dosage. Excessive Pine Oil may produce overly stable froth and affect concentrate drainage, while insufficient dosage may result in poor mineral recovery. A stepwise dosage test is recommended to determine the most suitable operating range for each ore type.
Q2. How does Pine Oil improve froth stability in mineral flotation?
Pine Oil improves flotation performance by reducing surface tension and promoting the formation of stable air bubbles in the froth zone. Its natural terpenoid components provide froth-forming properties that help maintain an appropriate froth layer for mineral attachment and recovery. The effectiveness of Pine Oil depends on factors such as mineral surface characteristics, collector chemistry, pulp pH, and water composition. During flotation testing, engineers typically evaluate froth persistence, bubble size, drainage behavior, and concentrate selectivity to optimize Pine Oil application. Proper control of froth stability is important to avoid excessive entrainment of gangue minerals.
Q3. How should Pine Oil performance be optimized in high-clay nickel ore flotation?
High-clay nickel ores often present challenges due to slime coating, unstable froth conditions, and reduced mineral selectivity. Pine Oil can be used as a frother to improve bubble formation and froth structure, but its dosage should be carefully controlled. Optimization usually involves combining frother adjustment with suitable dispersants or regulators to reduce the negative effects of fine clay particles. Laboratory tests should evaluate froth mobility, nickel recovery, concentrate grade, and gangue entrainment under different Pine Oil concentrations. The optimal condition depends on ore mineralogy, clay content, and the overall flotation reagent scheme.
Q4. What factors affect Pine Oil frothing performance under high calcium water conditions?
High calcium water may influence flotation chemistry by interacting with mineral surfaces, collectors, and other reagents. The frothing performance of Pine Oil under such conditions should be evaluated through controlled flotation tests using actual process water whenever possible. Important evaluation parameters include froth stability, bubble characteristics, concentrate quality, and recovery changes. Adjustments to reagent dosage, pulp conditioning time, or the use of complementary dispersing agents may be required depending on the mineral system. Pine Oil generally provides stable frothing properties, but site-specific water chemistry should always be considered during flotation reagent optimization.
Q5. How does Pine Oil compare with MIBC as a flotation frother?
Pine Oil and MIBC are widely used flotation frothers, but they have different froth characteristics. Pine Oil typically produces a stronger and more persistent froth due to its natural oil-based components, while MIBC generally provides a more selective and easily draining froth structure. The suitable choice depends on ore type, flotation objectives, and circuit requirements. For ores requiring stronger froth retention, such as some sulfide or complex ores, Pine Oil may provide advantages. For applications requiring faster froth collapse and improved concentrate cleanliness, MIBC may be preferred. Comparative laboratory testing is recommended before industrial application.
Q6. How does Pine Oil dosage influence flotation froth layer thickness?
Pine Oil concentration directly affects bubble generation, froth stability, and froth layer characteristics during flotation. Increasing dosage generally enhances froth formation and increases froth persistence, but excessive dosage may create a thick, highly stable froth that reduces drainage efficiency and increases gangue entrainment. Insufficient dosage may lead to weak froth formation and lower mineral recovery. Engineers typically optimize Pine Oil dosage by monitoring froth appearance, concentrate grade, recovery rate, and tailings losses during laboratory or pilot-scale testing. The appropriate dosage depends on ore mineralogy, pulp conditions, and the selected collector system.
Q7. What is the role of Pine Oil in copper-molybdenum flotation circuits?
In copper-molybdenum flotation, Pine Oil is mainly used to improve froth formation and maintain suitable froth conditions for valuable mineral recovery. It helps create stable air bubbles that support the attachment and transportation of hydrophobic mineral particles. However, frother selection and dosage must be balanced with collector performance, depressant usage, and pulp chemistry to maintain selectivity between valuable minerals and gangue. During process optimization, metallurgical engineers typically evaluate Pine Oil through rougher and cleaner flotation tests, focusing on recovery, concentrate grade, froth behavior, and downstream separation requirements.
Q8. How should Pine Oil be selected for flotation of complex ores containing fine particles?
Fine particle flotation often requires careful control of bubble size, froth stability, and mineral selectivity. Pine Oil can provide effective frothing properties for complex ore systems, but selection should consider the degree of mineral liberation, slime content, and reagent compatibility. For fine-grained ores, excessive froth stability may increase entrainment of unwanted minerals, while insufficient frothing may reduce recovery. Laboratory evaluation should include different Pine Oil dosages combined with collectors and modifiers to determine the optimal balance between recovery and concentrate quality. Process conditions such as pH, pulp density, and conditioning time should also be considered.
Q9. How does Pine Oil purity affect flotation froth quality?
The purity and composition of Pine Oil can influence froth consistency, bubble formation, and flotation repeatability. Higher-quality Pine Oil generally provides more predictable frothing behavior, while variations in composition may lead to differences in froth stability and reagent consumption. In industrial flotation operations, reagent quality control is important for maintaining stable metallurgical performance. Evaluation should include froth characteristics, concentrate recovery, reagent dosage requirements, and compatibility with other flotation chemicals. Selecting Pine Oil with consistent technical specifications helps improve process control and reduces fluctuations caused by frother quality variation.
Q10. What are the key factors when applying Pine Oil in industrial flotation plants?
The successful application of Pine Oil in flotation plants depends on proper matching of frother properties with ore characteristics and process conditions. Key factors include mineral type, particle size distribution, pulp pH, water chemistry, collector system, and flotation equipment design. Engineers should optimize Pine Oil dosage through laboratory testing, pilot trials, and continuous monitoring of froth behavior and metallurgical results. The objective is to achieve a stable but selective froth phase that supports valuable mineral recovery while minimizing unwanted gangue recovery. Technical evaluation under actual plant conditions is recommended for reliable process optimization.